
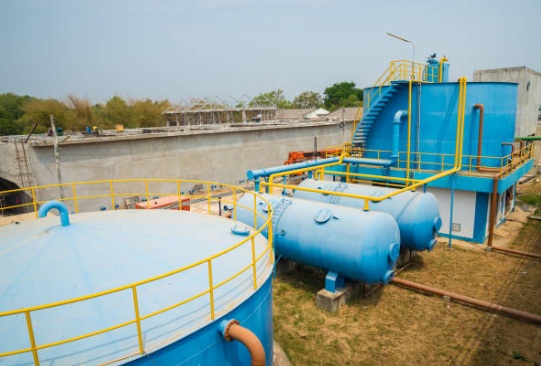
Sequential Batch Reactor (SBR) is an advanced activated sludge process in which all biological treatment stages—fill, aeration, reaction, settling and decanting—are carried out sequentially in a single reactor tank under controlled operating cycles.
Unlike conventional continuous flow systems, SBR operates in time-based cycles, making it highly effective for wastewater streams with fluctuating flow, variable organic load and intermittent discharge patterns.
The SBR process provides excellent removal efficiency for BOD, COD, suspended solids and nutrients such as ammonia, while eliminating the requirement of a separate secondary clarifier. Due to its flexibility and compact footprint, SBR technology is widely adopted for industries and facilities requiring consistent treated water quality and reuse-ready effluent.
Process Operation
A typical SBR cycle consists of the following stages:
Fill phase for controlled influent introduction
Aeration and reaction phase for biological oxidation and nitrification
Anoxic phase for denitrification (where required)
Settling phase for biomass separation
Decanting phase for clear treated water withdrawal
Cycle duration and phase sequencing are adjusted based on influent characteristics, load variation and treated water quality requirements.
How S N Group of Environment Delivers SBR Systems
At S N Group of Environment, SBR systems are engineered based on detailed wastewater analysis and site-specific operating conditions rather than generic cycle charts.
Our design philosophy focuses on long-term process stability, operational simplicity and regulatory compliance.
Engineering Strengths of Our SBR Design
Detailed analysis of influent flow and organic load variation before cycle finalization
Customized cycle programming to handle peak and low load conditions
Optimized aeration and anoxic phases to maintain stable MLSS, DO and F/M ratio
Selection of energy-efficient aeration systems for uniform oxygen transfer
Proper decanter selection, sizing and placement to prevent sludge carry-over
Automation and PLC logic designed for consistent compliance and reuse operation
Performance & Compliance Focus
Each SBR system is designed to deliver stable effluent quality with low operator dependency and minimal process intervention.
Our plants are engineered to consistently meet CPCB / SPCB discharge and reuse norms, ensuring inspection readiness and long-term regulatory compliance.
Key Advantages of SBR Technology
Excellent performance under fluctuating flow and load conditions
Compact layout with reduced civil footprint
No requirement of secondary clarifier
High treated water quality suitable for reuse applications
Flexible operation and easy process control
Reduced sludge handling complexity