
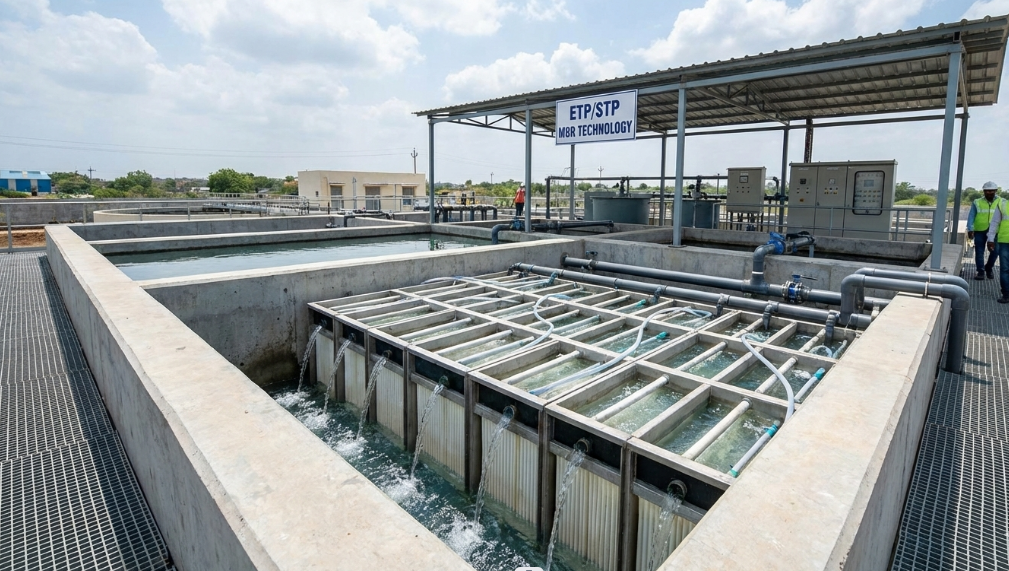
Membrane Bioreactor (MBR) is an advanced wastewater treatment technology that integrates biological treatment with membrane filtration, replacing the conventional secondary clarifier with microfiltration or ultrafiltration membranes.
This combination enables MBR systems to produce very high-quality treated water with extremely low TSS and turbidity, making the process ideal for 100% water recycling and reuse applications.
MBR systems operate at higher MLSS concentrations compared to conventional biological processes, allowing compact plant design while achieving superior effluent quality. Due to its consistent performance and small footprint, MBR technology is widely adopted for projects with stringent discharge norms, limited space availability and reuse-driven objectives.
Process Working Principle
In an MBR system, biological treatment is carried out in an aeration tank where organic matter is degraded by microorganisms. Instead of gravity settling, treated water is separated using membrane modules that act as a physical barrier, retaining biomass and suspended solids within the system.
The membranes ensure stable effluent quality irrespective of hydraulic or load fluctuations.
How S N Group of Environment Delivers MBR Systems
At S N Group of Environment, MBR systems are engineered as fully integrated treatment processes rather than simple membrane installations.
Our design approach focuses on long-term membrane performance, energy efficiency and operational reliability.
Engineering Strengths of Our MBR Design
Membrane selection based on wastewater characteristics, fouling tendency and reuse requirements
Design of effective pre-treatment systems to protect membranes and extend membrane life
Flux-based membrane sizing instead of nominal flow assumptions for stable long-term operation
Optimized MLSS and sludge age control for biological stability
Air scouring and backwash logic engineered to minimize energy and chemical consumption
Treated water quality aligned with reuse standards and RO feed water requirements
Performance & Compliance Focus
Our MBR systems are designed to deliver consistent treated water quality with minimal downtime and reduced operational challenges.
Each system is engineered to meet CPCB / SPCB discharge and reuse norms, ensuring inspection readiness and long-term regulatory compliance.
Key Advantages of MBR Technology
Very high treated water quality suitable for 100% reuse
Compact plant design with reduced footprint
Stable performance under fluctuating flow and load conditions
Elimination of secondary clarifier requirement
Consistent effluent quality for RO and advanced reuse systems
Reliable long-term operation with proper membrane protection