
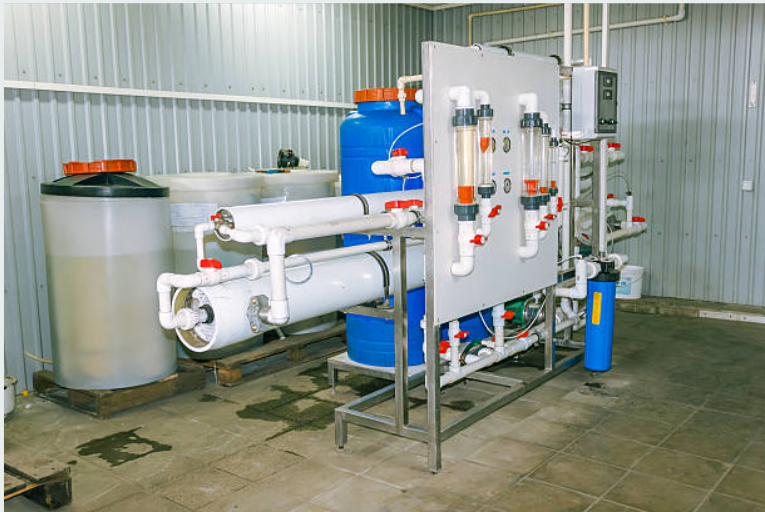
Reverse Osmosis (RO) is a pressure-driven membrane separation technology used for removal of dissolved salts (TDS), hardness, heavy metals and dissolved organic impurities from water.
RO membranes function as a molecular barrier, allowing only water molecules to pass through while rejecting contaminants, producing high-quality permeate suitable for industrial and reuse applications.
RO systems are widely adopted where consistent, low-TDS water quality is required, including water recycling, industrial process water and high-quality utility or wash water applications. A properly engineered RO system relies heavily on effective pretreatment and precise operating control to prevent fouling, scaling and membrane degradation.
Applications of RO Systems
Water recycling and reuse systems
Industrial process and utility water treatment
High-quality wash water applications
RO-based ZLD and high-recovery treatment systems
How S N Group of Environment Delivers RO Systems
At S N Group of Environment, RO systems are engineered as complete integrated treatment solutions rather than standalone membrane skids.
Our design philosophy emphasizes long membrane life, stable operation and optimized recovery with minimum operating cost.
Engineering Strengths of Our RO Design
Detailed feed water analysis to define system recovery, salt rejection and operating pressure
Design and integration of appropriate pretreatment systems such as UF, MGF, ACF and chemical dosing
Selection of RO membranes based on water chemistry, fouling tendency and reuse requirements
High-pressure pump selection optimized for energy efficiency and stable operation
Recovery optimization to reduce reject volume and overall water loss
Instrumentation and control design for performance monitoring and system protection
Performance & Compliance Focus
Our RO systems are designed to deliver consistent permeate quality suitable for critical reuse and process applications.
Each system is engineered to meet CPCB / SPCB reuse and discharge norms when integrated into water recycling schemes.
Key Advantages of RO Technology
Effective removal of dissolved salts and hardness
High-quality permeate for industrial and reuse applications
Stable and predictable system performance
Optimized recovery and reduced reject generation
Extended membrane life through proper pretreatment and control
Energy-efficient operation with optimized system design