
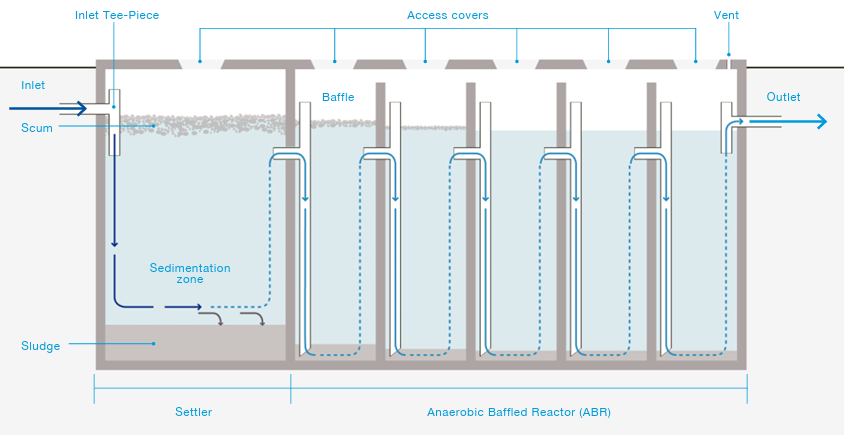
Anaerobic Baffled Reactor (ABR) is an advanced anaerobic wastewater treatment technology in which wastewater flows through a series of baffled compartments arranged in alternating upflow and downflow patterns.
Each baffled chamber functions as an independent biological zone, ensuring enhanced contact between wastewater and anaerobic biomass, resulting in improved treatment efficiency and process stability.
ABR technology offers excellent shock load resistance, reliable organic load reduction and very low energy consumption, as the process operates without aeration. Due to its robust performance, ABR is commonly used as a primary biological treatment stage followed by aerobic polishing to achieve final discharge or reuse standards.
Process Working Principle
Influent wastewater enters the reactor and sequentially passes through multiple baffled chambers.
In each chamber, anaerobic microorganisms degrade organic matter while biomass remains retained within the system.
The staged treatment approach improves overall COD reduction and process resilience under fluctuating operating conditions.
How S N Group of Environment Delivers ABR Systems
At S N Group of Environment, ABR systems are engineered using a hydraulics-first and process-stability-focused design philosophy rather than standard compartment layouts.
Our designs ensure uniform flow distribution, stable anaerobic digestion and effective integration with downstream treatment processes.
Engineering Strengths of Our ABR Design
Chamber-wise Hydraulic Retention Time (HRT) distribution for controlled and stable anaerobic digestion
Baffle design optimized to eliminate short-circuiting and dead zones
Controlled flow velocity to ensure biomass retention and process efficiency
Robust civil and hydraulic design for long-term operational reliability
Provision for odour control and gas venting
Seamless integration with aerobic and tertiary treatment systems for final polishing
Performance & Compliance Focus
Our ABR systems are designed to deliver consistent pretreatment performance with minimal operational intervention.
Each system supports downstream treatment efficiency and assists in achieving CPCB / SPCB discharge and reuse norms when combined with appropriate post-treatment stages.
Key Advantages of ABR Technology
High stability under fluctuating organic and hydraulic loads
Very low energy and operational cost
Excellent shock load resistance
Reduced sludge generation compared to aerobic systems
Strong pretreatment for high-strength wastewater
Improved performance of downstream aerobic treatment units